High-Frequency Vibrating Screen for Fermented Milk Processing in Singapore
Background
A food manufacturer based in Singapore approached us with an application: processing fermented milk. After refrigeration, the product takes on a texture similar to yogurt, while at room temperature it becomes slightly watery. Apart from the culture granules that need to be filtered out, the material contains no solid matter.
Key Requirements
- Capacity: 50 liters per hour
- Precision: 1.5 mm to 2.5 mm mesh
- Material: Food-grade construction
Because the viscosity of the material may vary with temperature, the required vibration and power parameters could be relatively complex. The client needed a solution capable of reliable solid-liquid separation under these changing conditions.
Our Recommendation
We recommended the 600-type high-frequency vibrating screen, which achieves effective solid-liquid separation through the combined action of pressure and vibration. This configuration is well suited to handling materials with variable viscosity while maintaining the required filtration precision.
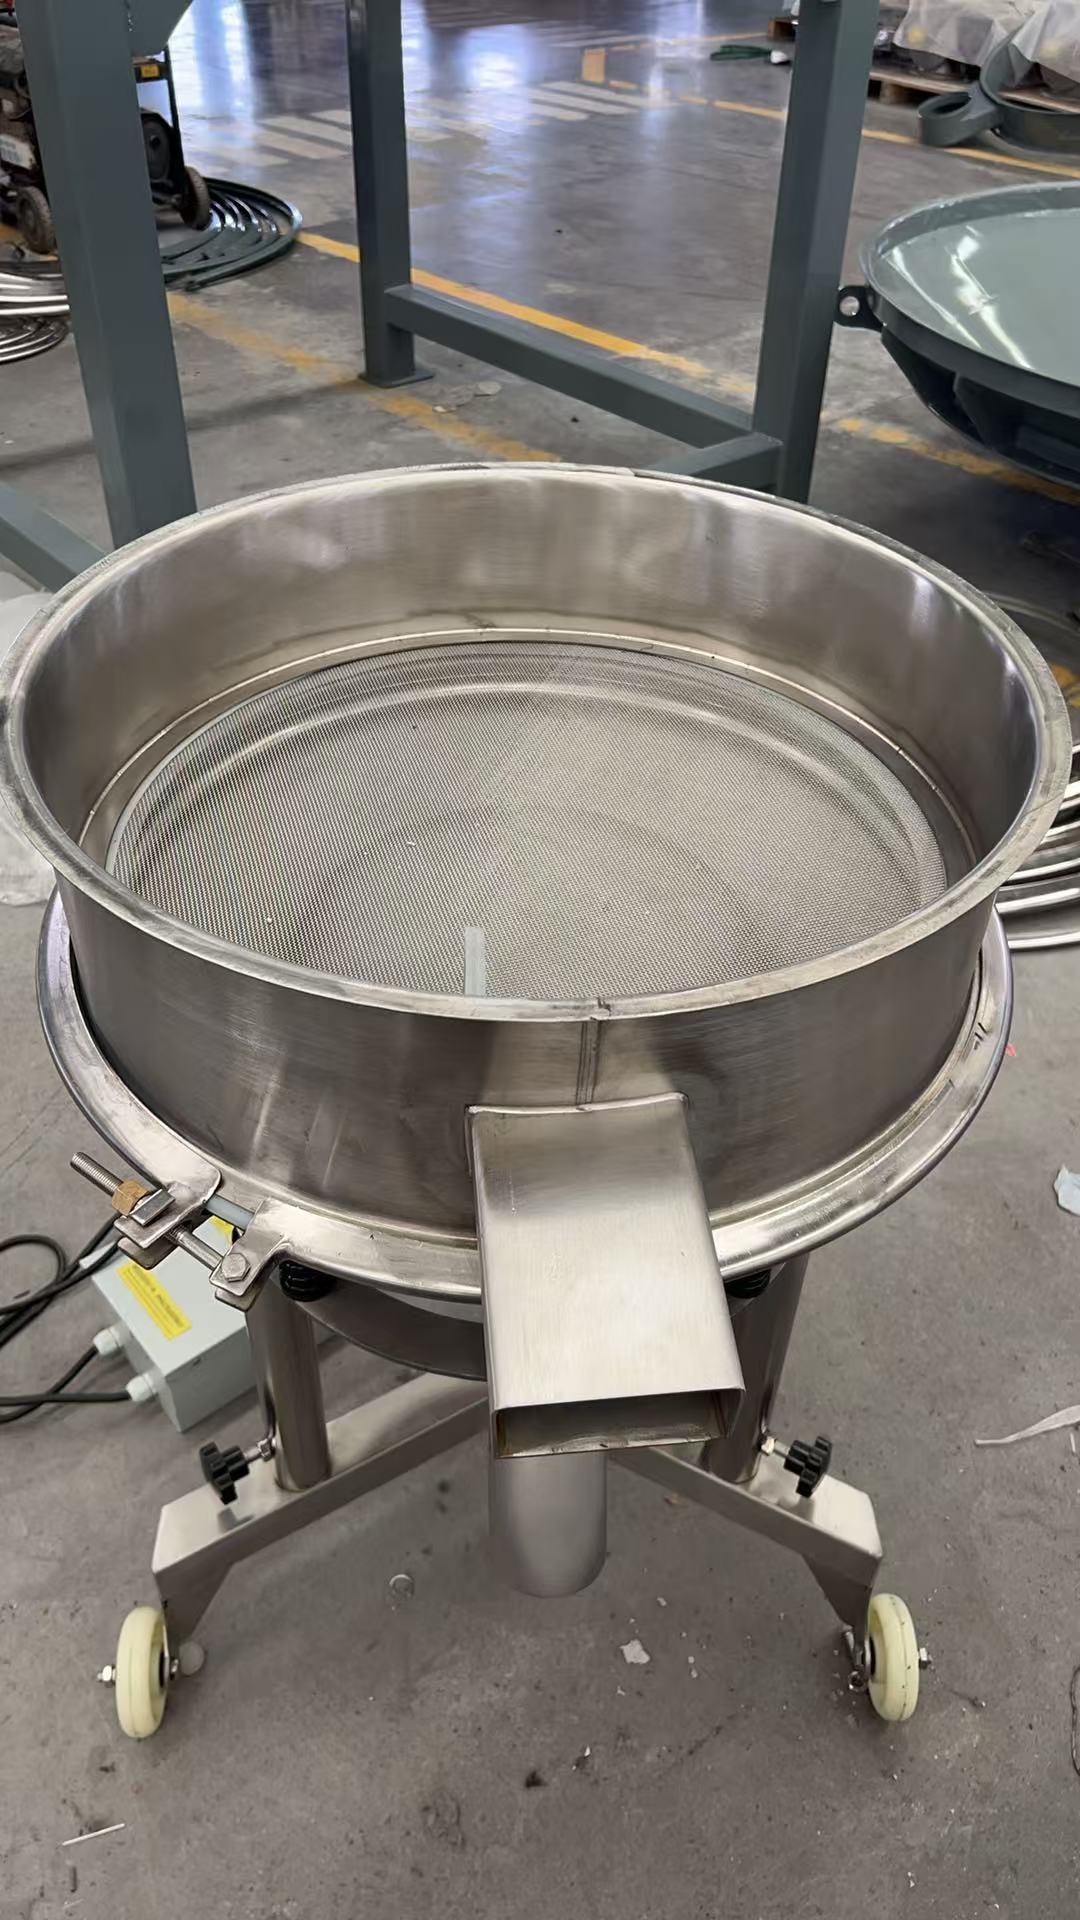
On-Site Trial
The client later visited our factory in person to conduct a trial run with their own material.
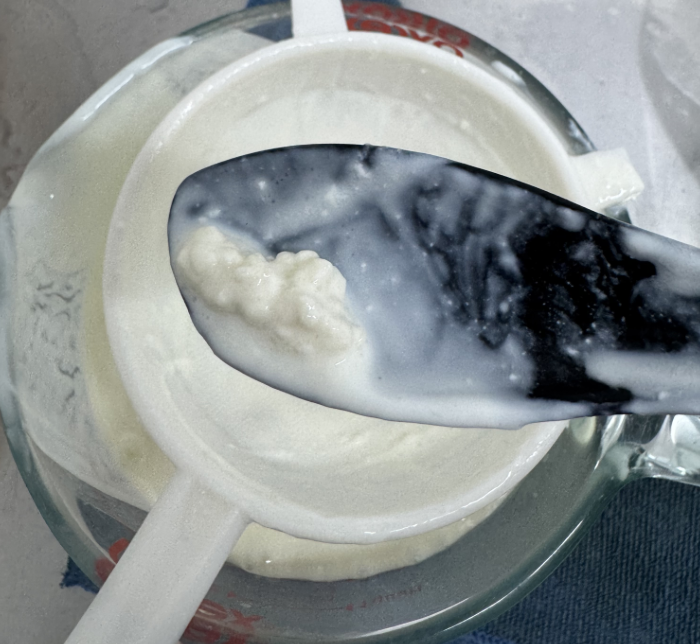
The trial allowed us to verify performance with the actual product and fine-tune the parameters to match the client's processing conditions.
Conclusion
This application demonstrates that vibrating screens are not limited to handling dry solids. With the right configuration and parameters, they can also be an effective solution for liquid and semi-liquid materials — including challenging food applications where viscosity varies with temperature.
If you are dealing with similar solid-liquid separation challenges, or would like to explore whether a vibrating screen is suitable for your liquid processing needs, we welcome you to contact us for a consultation. Our team would be glad to help you find the right solution.